Industrial Electrical Troubleshooting: How Experts Think Differently
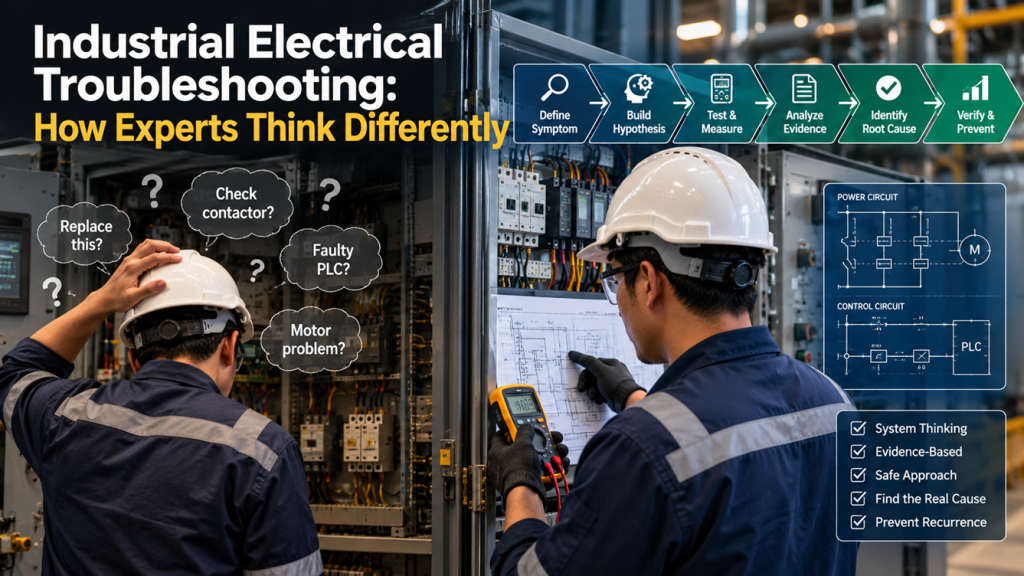
When an industrial electrical system fails, the difference between a beginner and an expert is rarely the ability to use a multimeter.
Both may know how to measure voltage.
Both may understand electrical drawings.
Both may know how contactors, relays, motors, breakers, VFDs, PLCs, and protection systems operate.
The difference often lies somewhere deeper:
Experts think differently about the problem.
They do not immediately ask:
“Which component should I replace?”
Instead, they ask:
“What evidence do I have, what conditions must exist for this symptom to occur, and what is the fastest safe way to eliminate possible causes?”
Industrial electrical troubleshooting is therefore not simply a technical activity.
It is a structured process of observation, hypothesis, measurement, elimination, verification, and learning.
And the quality of that thinking often determines whether a fault is resolved in 20 minutes—or turns into several hours of unnecessary component replacement.
Troubleshooting Is Not Guessing Faster
In many plants, troubleshooting begins when production is already under pressure.
A motor will not start.
A breaker trips repeatedly.
A VFD shows a fault.
A PLC output is active but the field device does not operate.
A protection relay initiates an unexpected trip.
Operations wants the equipment back online immediately.
Under these conditions, inexperienced troubleshooters can easily fall into a familiar pattern:
symptom → assumption → component replacement
For example:
Motor does not start → contactor must be faulty → replace contactor.
Sometimes this works.
But when it does, the troubleshooter may simply have been lucky.
A systematic troubleshooter uses another sequence:
symptom → evidence → possible causes → tests → elimination → root cause → verification
That difference may appear small.
In practice, it changes everything.
1. Experts Start With the System, Not the Component
A common troubleshooting mistake is focusing too quickly on the component closest to the symptom.
Suppose a motor fails to start.
The obvious suspect might be the motor starter.
But the complete starting chain could involve:
Power Supply
↓
Circuit Breaker
↓
Contactor
↓
Overload Protection
↓
Motor Cable
↓
Motor
while the control chain could be:
Control Power
↓
Emergency Stop
↓
Permissives
↓
PLC Logic
↓
Output Module
↓
Interposing Relay
↓
Contactor Coil
And there may also be process interlocks such as:
Low suction pressure
High temperature
Low lubrication pressure
Valve not open
Equipment permissive not satisfied
An expert therefore does not initially troubleshoot the motor.
They troubleshoot the system responsible for allowing the motor to operate.
This systems-level thinking prevents tunnel vision.
2. Experts Define the Symptom Precisely
Compare these two statements:
“The pump is not working.”
and:
“The pump motor receives a start command from the DCS, but the contactor does not energize.”
The second statement dramatically reduces the troubleshooting space.
A good troubleshooter continuously converts vague symptoms into precise technical observations.
Instead of:
“The breaker has a problem.”
They might establish:
“The breaker trips instantaneously during motor acceleration.”
Instead of:
“The VFD is unstable.”
They may identify:
“DC bus overvoltage occurs during deceleration.”
Instead of:
“The transmitter is faulty.”
They might determine:
“The transmitter locally indicates 65%, while the DCS continuously receives 4 mA.”
The more precise the symptom, the smaller the fault domain becomes.
3. Experts Separate Facts From Assumptions
This is one of the most important troubleshooting disciplines.
Imagine someone says:
“The motor tripped because it was overloaded.”
That may sound reasonable.
But is it a fact?
Or an interpretation?
A structured troubleshooter separates them.
Facts
- Motor current reached 142 A.
- Rated current is 110 A.
- Overload relay operated.
- Bearing temperature was normal.
- Process flow increased shortly before the trip.
Hypothesis
The motor experienced excessive mechanical loading.
These are not the same.
The overload trip proves that excessive current existed.
It does not automatically prove why.
Possible causes could include:
- mechanical overload,
- locked or partially restricted equipment,
- low voltage,
- phase imbalance,
- single phasing,
- incorrect overload settings,
- motor winding problems,
- process conditions.
Experts avoid treating hypotheses as facts.
That prevents premature conclusions.
4. Experts Think in Terms of Cause-and-Effect Chains
Industrial equipment failures rarely exist in isolation.
A problem often develops through a sequence.
For example:
Loose electrical connection
→ increased resistance
→ localized heating
→ insulation degradation
→ phase imbalance
→ increased motor current
→ overload trip
If troubleshooting stops at:
“Overload relay operated,”
the root cause remains hidden.
Expert troubleshooters therefore ask:
What happened immediately before this event?
and:
What physical mechanism could connect these observations?
This causal thinking is particularly important for recurring failures.
5. Experts Use Hypotheses, Not Random Checks
Random troubleshooting often looks productive because technicians remain busy.
They measure many points.
They reset devices.
They replace components.
They inspect cabinets.
But activity does not necessarily equal progress.
Experts normally develop a short list of probable hypotheses.
Suppose a contactor will not energize.
Potential causes may be:
- no control power,
- open emergency-stop circuit,
- missing process permissive,
- PLC output inactive,
- output module failure,
- interposing relay failure,
- open wiring,
- defective contactor coil.
Each measurement should eliminate one or more hypotheses.
For example:
Voltage present across contactor coil terminals?
Yes
The control circuit is likely functioning up to that point.
Focus on:
- contactor coil,
- mechanism,
- coil voltage rating,
- mechanical obstruction.
No
Move upstream in the control circuit.
One measurement has divided the fault tree into two major branches.
That is efficient troubleshooting.
6. Experts Measure at the Point With the Highest Information Value
Beginners sometimes make measurements simply because the test point is accessible.
Experts choose measurements strategically.
Consider this control circuit:
24 VDC Supply
→ Fuse
→ E-Stop
→ PLC Contact
→ Relay
→ Contactor Coil
→ 0 V
Testing voltage only at the power supply tells very little.
Testing directly across the contactor coil during a start command gives significantly more information.
If 24 VDC is present but the contactor does not operate, much of the upstream circuit can immediately be eliminated.
The best measurement is not always the easiest measurement.
It is the one that reduces uncertainty most quickly.
7. Experts Understand Normal Before Diagnosing Abnormal
Troubleshooting becomes much easier when you understand how the system should operate.
Before searching for faults, experienced troubleshooters often establish:
- normal voltage,
- normal current,
- expected sequence,
- permissive conditions,
- protection settings,
- normal temperatures,
- normal vibration,
- typical starting time,
- expected PLC states,
- normal process conditions.
Without a model of normal operation, abnormal behavior is difficult to recognize.
This is one reason experienced technicians often troubleshoot familiar equipment faster.
They possess a mental baseline.
The goal for developing troubleshooters should therefore not only be to study failures.
It should also be to understand normal system behavior in depth.
8. Experts Read Drawings as Logic Maps
Electrical drawings are not merely documentation.
During troubleshooting, they are maps of possible failure paths.
An experienced troubleshooter may use:
- single-line diagrams,
- schematic diagrams,
- wiring diagrams,
- interconnection diagrams,
- loop diagrams,
- terminal drawings,
- cause-and-effect charts,
- PLC logic,
- protection logic diagrams.
Suppose the motor starter coil is not receiving voltage.
Instead of physically following every cable, the troubleshooter may follow the schematic:
Control fuse → E-stop contact → overload auxiliary → PLC output → interposing relay → terminal block → coil
The drawing transforms an apparently complex cabinet into a logical sequence.
Each point becomes a troubleshooting checkpoint.
9. Experts Understand That Electrical Faults Can Be Mechanical or Process-Related
One of the biggest mistakes in industrial troubleshooting is assuming an electrical symptom must have an electrical cause.
A motor overload may result from:
- pump blockage,
- bearing seizure,
- excessive process flow,
- misalignment,
- compressor loading,
- valve position,
- mechanical binding.
Similarly, a VFD overcurrent alarm might originate from:
- motor problems,
- cable insulation issues,
- acceleration settings,
- mechanical overload,
- process disturbances.
Industrial systems are interconnected.
Experts therefore expand their thinking beyond electrical boundaries.
They ask:
Is the electrical system failing, or is it correctly responding to another problem?
This question is extremely powerful.
Sometimes a protective device trip is not the fault.
It is the system doing exactly what it was designed to do.
10. Experts Never Treat Protection as an Obstacle
When production pressure increases, there may be a temptation to bypass protection.
This is dangerous thinking.
A relay trip, interlock, overload, or breaker operation is information.
The first question should not be:
“How can we reset it?”
It should be:
“Why did it operate?”
A protection device generally indicates that a defined condition occurred.
For example:
- overcurrent,
- earth fault,
- overload,
- undervoltage,
- differential current,
- overtemperature,
- phase imbalance.
Resetting without understanding the cause can remove the symptom temporarily while allowing the underlying condition to become more severe.
11. Experts Prioritize Safety Before Diagnosis
Troubleshooting electrical equipment may expose personnel to:
- electric shock,
- arc flash,
- arc blast,
- unexpected equipment movement,
- stored electrical energy,
- stored mechanical energy,
- process energy.
Therefore, troubleshooting methodology must always begin with risk assessment and applicable safe-work practices.
OSHA’s hazardous-energy requirements, for example, require energy-control procedures where unexpected energization or release of stored energy could cause injury.
Electrical safety frameworks such as NFPA 70E similarly emphasize risk controls around electrical work, including energized-work considerations.
The important principle is:
Production urgency never changes electrical physics.
Before performing measurements, technicians must establish whether the work can be performed de-energized and apply the appropriate isolation, verification, PPE, permits, and procedures required by their facility and jurisdiction.
An expert troubleshooter is not the person who takes the greatest risk.
It is the person who obtains the required information while controlling risk effectively.
12. Experts Understand the Difference Between “No Voltage” and “No Usable Voltage”
Suppose a technician measures 230 V.
They may conclude:
“The supply is good.”
But voltage alone may not prove the supply can deliver current.
A degraded connection might still produce a normal unloaded voltage.
Once the load is applied, the voltage may collapse.
Therefore experts often evaluate electrical conditions dynamically.
They may compare:
- no-load versus loaded voltage,
- phase-to-phase voltage,
- phase-to-neutral voltage,
- voltage drop across contacts,
- phase currents,
- current imbalance,
- source voltage versus load voltage.
Sometimes the most useful measurement is not:
“Is voltage present?”
but:
“What happens to voltage when the system attempts to operate?”
13. Experts Compare Phases Instead of Looking at One Number
Three-phase systems provide a powerful troubleshooting advantage:
each phase can act as a reference for the others.
Suppose a motor current measurement shows:
| Phase | Current |
|---|---|
| L1 | 82 A |
| L2 | 83 A |
| L3 | 54 A |
The absolute current may appear acceptable.
But the imbalance is highly informative.
Similarly:
| Voltage | Value |
|---|---|
| L1-L2 | 400 V |
| L2-L3 | 398 V |
| L3-L1 | 401 V |
suggests a relatively balanced supply.
Experts therefore look for relationships, not simply individual values.
Patterns often reveal more than absolute numbers.
14. Experts Use Trend Data, Not Only Instantaneous Measurements
Many failures cannot be understood from a single measurement after the event.
Modern industrial plants often contain valuable historical information in:
- DCS historians,
- SCADA systems,
- protection relays,
- VFD event logs,
- power meters,
- motor protection relays,
- condition monitoring systems,
- PLC diagnostics.
Imagine a motor trips at 14:27.
Instead of immediately opening the panel, an expert might first review:
- current before trip,
- voltage,
- process load,
- temperature,
- vibration,
- operating state,
- alarms,
- sequence of events.
A trend might show:
current gradually increasing for 30 minutes before overload trip.
That tells a very different story from:
current suddenly jumping from normal to six times rated current.
The first suggests progressive loading.
The second may indicate a fault or locked condition.
Historical data transforms troubleshooting from reconstruction to evidence-based diagnosis.
15. Experts Pay Attention to What Changed
A highly effective troubleshooting question is:
What changed?
Many failures occur shortly after some change, including:
- maintenance,
- equipment replacement,
- software modification,
- PLC logic change,
- protection setting change,
- process modification,
- shutdown,
- cable termination work,
- instrument calibration.
For example:
Motor protection begins tripping after maintenance.
Possible investigation:
What was touched during maintenance?
Perhaps:
- a current transformer wire was disturbed,
- a cable termination became loose,
- motor leads were reconnected incorrectly,
- overload parameters were changed.
Recent change is not proof of causation.
But it is often a high-value investigative clue.
16. Experts Distinguish Root Cause From Failed Component
Suppose a contactor coil is burned.
Replacing the contactor solves the immediate problem.
But why did the coil burn?
Possible causes include:
- incorrect coil voltage,
- undervoltage causing chatter,
- overvoltage,
- mechanical obstruction,
- excessive switching frequency,
- unstable control supply,
- contamination.
The failed contactor is the failure location.
It may not be the failure cause.
This distinction separates repair from reliability improvement.
A repair restores operation.
Root cause analysis prevents recurrence.
17. Experts Verify the Repair
Troubleshooting does not end when equipment starts.
Consider a technician who replaces a fuse.
The machine operates again.
Is the problem solved?
Perhaps.
But perhaps an intermittent short circuit remains.
Experts verify the condition after repair.
Verification may include:
- checking operating current,
- checking voltage balance,
- monitoring temperature,
- confirming protection settings,
- checking alarms,
- running the equipment under normal load,
- reviewing trends,
- repeating several operating cycles.
The question becomes:
“Did we remove the cause, or only restore operation?”
18. Experts Know When to Stop Testing
Testing itself can introduce risk.
Excessive manipulation of equipment can:
- create new faults,
- disturb intermittent failures,
- increase arc-flash exposure,
- damage terminals,
- interrupt production,
- erase fault evidence.
Experts therefore avoid unnecessary testing.
Once sufficient evidence exists to establish the likely fault, the next step should be deliberate.
Good troubleshooting is not about collecting the maximum amount of data.
It is about collecting enough high-quality data to make the correct decision.
19. Experts Preserve Evidence
One of the worst troubleshooting practices is immediately resetting everything.
Resetting may erase:
- relay fault records,
- VFD fault histories,
- PLC states,
- sequence-of-event information,
- latched alarms.
Before resetting, experienced troubleshooters may document:
- fault codes,
- relay targets,
- alarm timestamps,
- equipment state,
- current,
- voltage,
- process conditions.
In difficult intermittent failures, the first event may contain the best evidence you will ever receive.
20. Experts Troubleshoot Probability, Not Every Possibility Equally
A breaker trip could theoretically result from dozens of causes.
But not all causes have equal probability.
Experts use information such as:
- failure history,
- operating conditions,
- equipment age,
- recent maintenance,
- environmental conditions,
- known failure modes.
For example, after heavy rain, a ground fault on outdoor equipment may be more probable than a spontaneous relay calibration failure.
This does not mean assumptions should replace measurements.
It means probabilities should guide the testing sequence.
A good troubleshooter tests the most probable and most informative causes first.
A Practical Expert Troubleshooting Framework
A useful industrial troubleshooting sequence is:
Step 1 — Make the Situation Safe
Understand the hazards.
Apply required isolation, permits, risk controls, PPE, and safe electrical work procedures.
Step 2 — Define the Problem
Describe exactly what the equipment is doing—and what it should be doing.
Step 3 — Collect Evidence
Review:
- alarms,
- operator reports,
- trends,
- fault records,
- protection indications,
- maintenance history.
Step 4 — Understand the System
Review drawings, logic, control philosophy, and operating sequence.
Step 5 — Establish Possible Causes
Develop several technically plausible hypotheses.
Step 6 — Prioritize Hypotheses
Rank them based on:
- probability,
- evidence,
- safety,
- testability.
Step 7 — Test Strategically
Choose measurements that eliminate the largest number of possibilities.
Step 8 — Isolate the Fault
Narrow the system until the faulty function, circuit, component, or external condition is identified.
Step 9 — Correct the Cause
Do not simply replace damaged components if another condition caused their failure.
Step 10 — Verify
Confirm proper operation under realistic operating conditions.
Step 11 — Document
Record:
- symptoms,
- findings,
- measurements,
- cause,
- corrective action,
- recommendations.
Example: Motor Will Not Start
Imagine the following complaint:
“Motor M-101 cannot start.”
A weak troubleshooting approach might be:
- reset overload,
- replace relay,
- replace contactor,
- inspect motor,
- call engineering.
An expert approach would first define the sequence.
Question 1
Is the start command actually being generated?
If no:
Troubleshoot upstream logic.
If yes:
Proceed.
Question 2
Is the PLC output active?
If no:
Check permissives and logic.
If yes:
Proceed.
Question 3
Is voltage reaching the interposing relay?
If yes but relay does not operate:
Investigate relay.
If no:
Investigate wiring or output circuit.
Question 4
Does the contactor coil receive rated voltage?
If yes but contactor does not pull in:
Investigate coil or mechanical mechanism.
If no:
Investigate upstream control circuit.
In only a few strategic checks, a complex starting system can be divided into manageable sections.
Example: Motor Overload Trips Repeatedly
Now consider another problem:
“Motor overload trips every few hours.”
Replacing the overload relay might restore operation temporarily.
But an expert may investigate:
Electrical
- phase current,
- voltage balance,
- current imbalance,
- loose connections,
- insulation condition.
Mechanical
- bearing condition,
- alignment,
- driven-equipment resistance,
- lubrication.
Process
- flow,
- pressure,
- loading,
- valve condition.
Protection
- overload setting,
- motor service factor,
- thermal model,
- trip class.
Historical
- when did the behavior start?
- what changed?
- does loading increase gradually?
- is the problem temperature dependent?
Troubleshooting becomes a multidisciplinary investigation rather than component replacement.
Troubleshooting Skill Grows Through Structured Thinking
Experience remains extremely important.
A technician who has seen hundreds of failures develops valuable pattern recognition.
But experience becomes dangerous if it turns into:
“I have seen this before, so I already know the answer.”
The expert mindset is different:
“This resembles a failure I have seen before, so that hypothesis deserves priority—but I still need evidence.”
That subtle difference protects experienced professionals from confirmation bias.
Pattern Recognition + First Principles
The strongest troubleshooters use two complementary approaches.
Pattern Recognition
Experience allows them to recognize familiar symptoms quickly.
First-Principles Reasoning
Electrical fundamentals allow them to reconstruct unfamiliar problems logically.
Pattern recognition creates speed.
First-principles reasoning provides resilience when the problem is new.
Experts combine both.
From Troubleshooter to Reliability Professional
Troubleshooting becomes even more valuable when its lessons are converted into organizational learning.
After a significant fault, ask:
- Could this failure happen elsewhere?
- Should preventive maintenance change?
- Should monitoring be added?
- Should protection settings be reviewed?
- Should the design be improved?
- Should spare-parts strategy change?
- Should technicians receive additional training?
At this point troubleshooting evolves into reliability engineering.
The organization moves from:
Repairing failures
to:
Preventing recurrence
and eventually toward:
Predicting failures before they interrupt production.
The Real Difference Between Beginners and Experts
Expert troubleshooters are not experts because they know every fault.
No one does.
They are experts because they know how to approach faults they have never seen before.
They:
- define problems precisely,
- distinguish facts from assumptions,
- understand system behavior,
- build hypotheses,
- prioritize probabilities,
- select high-value measurements,
- use drawings and historical data,
- think across electrical, mechanical, and process boundaries,
- respect protection systems,
- manage electrical risk,
- identify root causes,
- verify corrective actions,
- and preserve lessons for the future.
Their greatest tool is therefore not the multimeter.
It is their method of thinking.
And that method can be learned.
Build Troubleshooting Competency, Not Just Troubleshooting Experience
Every equipment failure provides an opportunity to develop technical competency.
Do not simply ask:
“What component failed?”
Ask:
“What evidence revealed the failure?”
“What mechanism caused it?”
“What measurement proved it?”
“Why did the protection respond?”
“How can recurrence be prevented?”
Professionals who repeatedly ask these questions develop more than troubleshooting experience.
They develop the structured judgment required to solve increasingly complex industrial problems.
And that is one of the key differences between someone who repairs electrical equipment and someone who becomes a true industrial electrical expert.
References and Safety Basis
Industrial troubleshooting activities should always be performed under applicable company procedures, local regulations, and electrical safety requirements. OSHA’s hazardous-energy standards establish requirements for controlling unexpected energization and stored energy during servicing and maintenance.
For electrical work, NFPA 70E provides a widely used framework for electrical safety-related work practices, including energized-work risk controls.
These requirements reinforce an important principle of professional troubleshooting:
A technically correct diagnosis is not competent troubleshooting unless it is achieved safely.